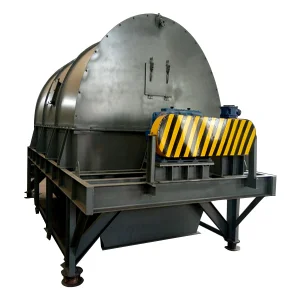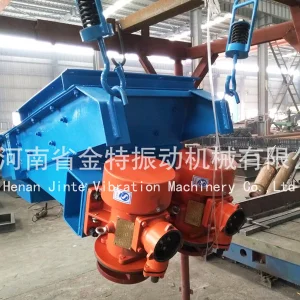
Annaba stands as a premier industrial and metallurgical powerhouse in North Africa. Driven by massive steel production, mineral extraction, and infrastructural development, the demand for high-efficiency crushers, vibrating screens, and heavy-duty conveying systems has reached an all-time high. Henan Jinte Technology Co., Ltd. delivers state-of-the-art machinery engineered to withstand harsh desert and coastal operating environments.
Our strategic focus for the Annaba market centers on lowering operational expenditure (OPEX) while maximizing throughput in aggregate processing and ore dressing plants.
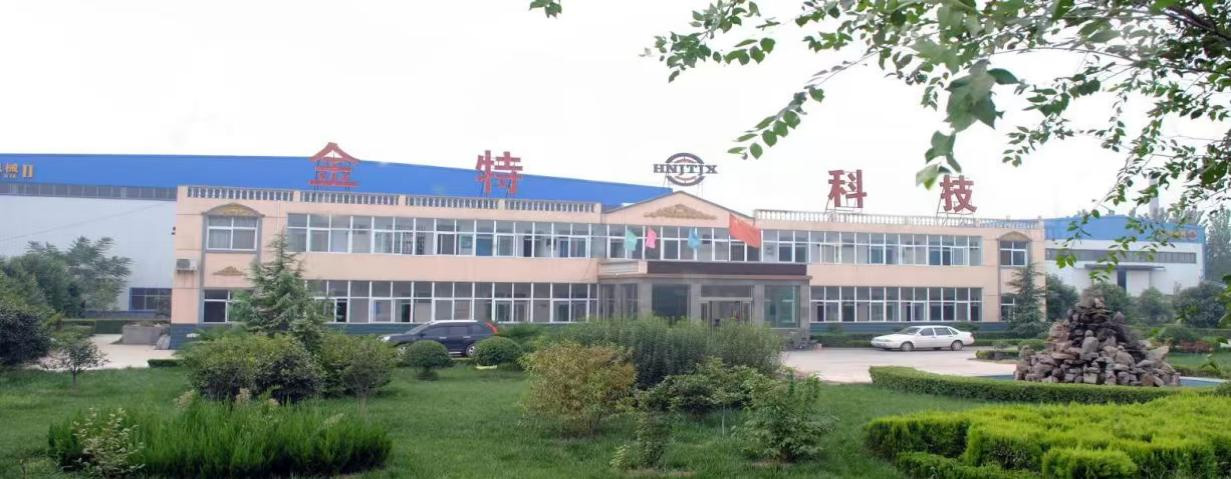
Henan Jinte Technology Co., Ltd. was officially registered and established in 2018. It has now developed into a mid-to-large-scale international enterprise specializing in the design and production of complete screening equipment, vibration equipment, and conveying products for sand and gravel production lines. The company also engages in machinery manufacturing, as well as the import and export of goods and technology.
Our company's products are exported to countries such as Iran, India, Central Africa, Algeria (Annaba region), and Asia. The design of our products emphasizes the concepts of environmental protection and energy efficiency, with current technical standards meeting international benchmarks and maintaining a leading position in the vibration machinery industry.
Located in Xinxiang Economic Development Zone, Henan, China, our 26,000-square-meter facility houses over 80 sets of advanced processing equipment. This includes vertical CNC machining centers, automatic flame cutters, CNC bending/shearing units, and automated shot-blasting equipment capable of handling single-lift loads exceeding 20 tons.
Using CXAX 3D design software and finite element analysis (FEA), our engineering team simulates extreme stress conditions to ensure structural integrity, wear resistance, and long lifecycle for all crushers delivered to Annaba.
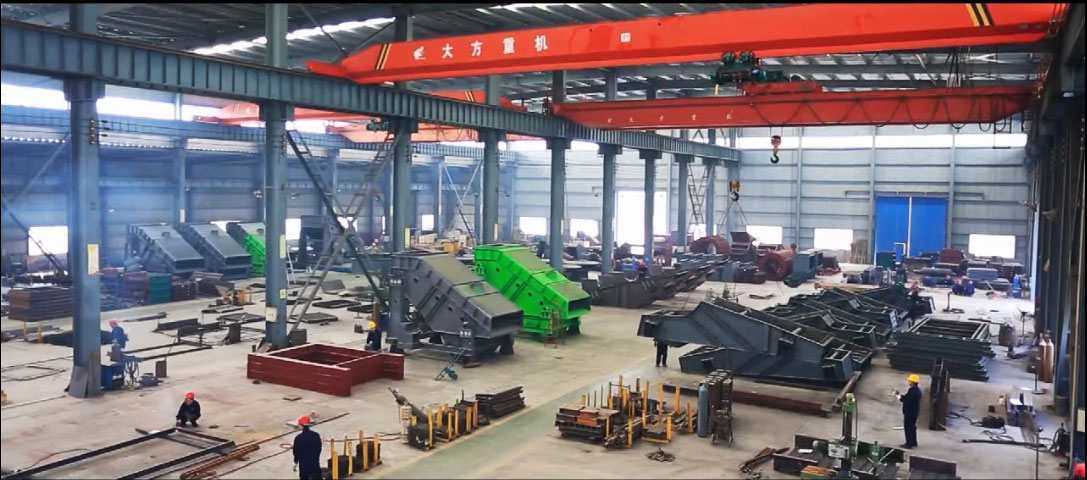
Our company mainly produces vibrating screens, crushers, and supporting complete sets of equipment widely used in metallurgy, electric power, mining, coal, sand and stone, chemical industry, ceramics, and tailing processing lines.
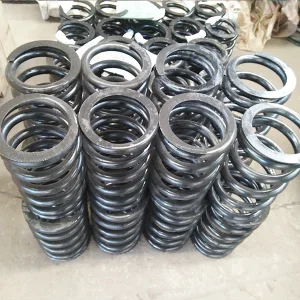
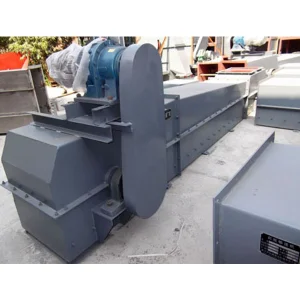
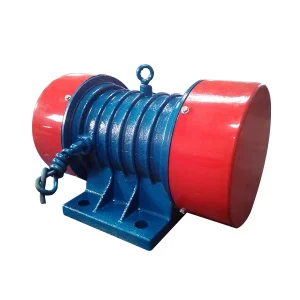
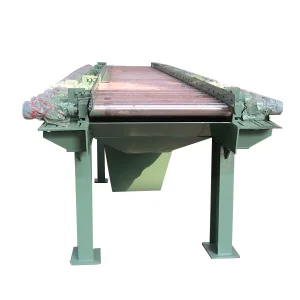
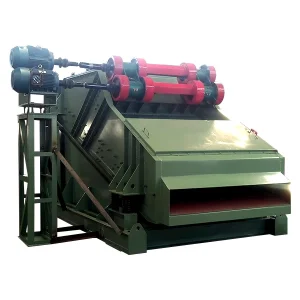
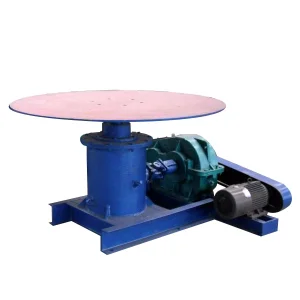
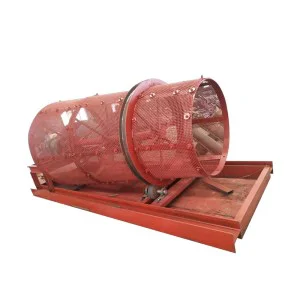
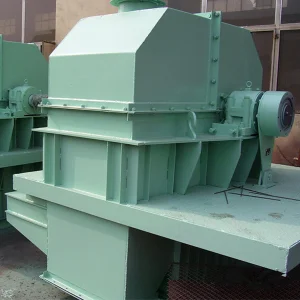
Including sandstone complete equipment, environmentally friendly sintered vibrating screens, supporting belt conveyors, mixing machines, unit composite vibrating screens, high-efficiency heavy-duty vibrating screens, large circular vibrating screens, double-axis/three-axis self-synchronizing elliptical screens, probable rod screens, feeders, electromagnetic feeders, disc feeders, reciprocating coal feeders, vibrating conveyors, bucket elevators, vibration motors, linear self-vibration sources, industrial crushers, and composite springs.
As one of the basic equipment industries, screening and crushing machinery is primarily used in smelting sintering, raw material grading, and aggregate production. By optimizing separation efficiency, material consumption and environmental pollution are significantly reduced—fully aligning with international green industrial standards.
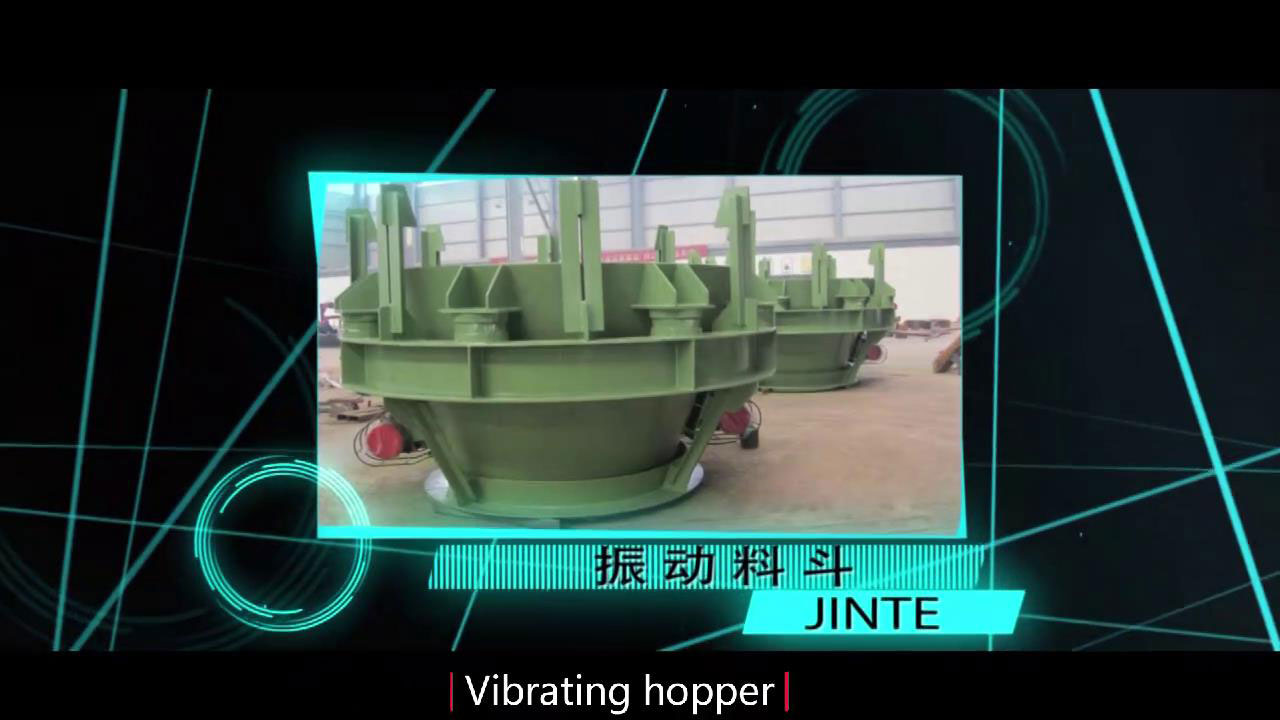
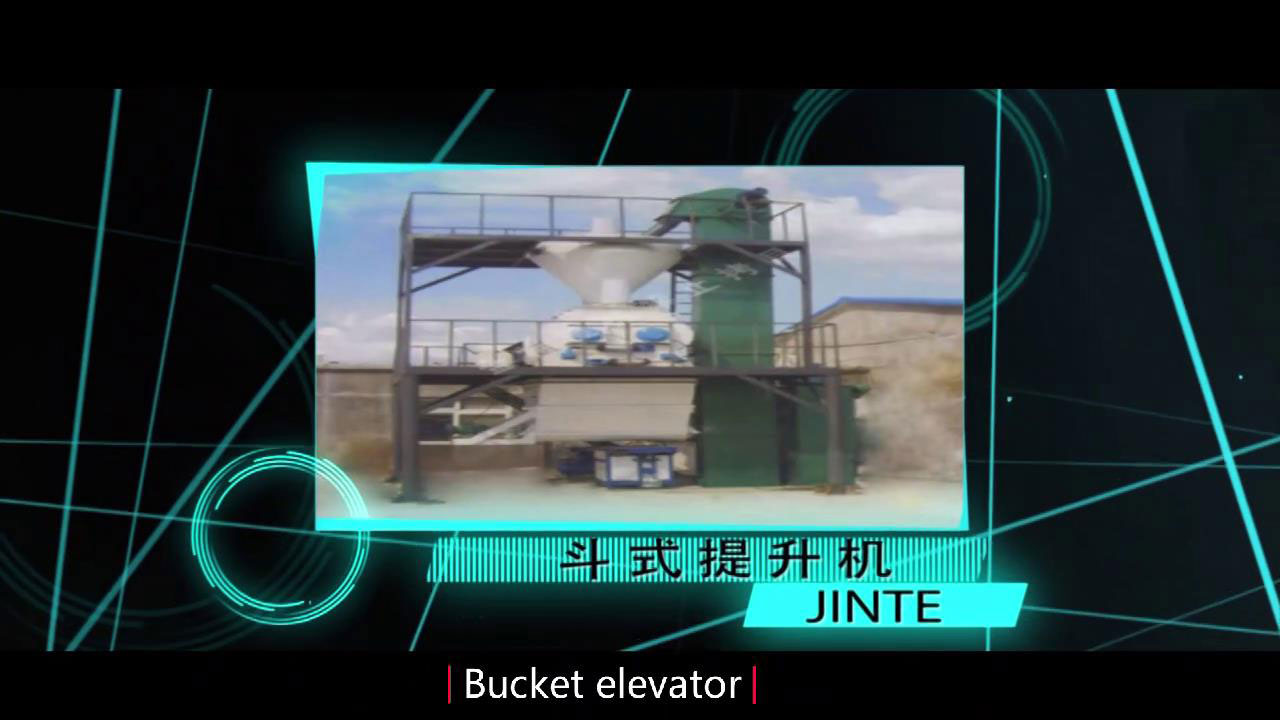
Our crushers are engineered with high-manganese alloy steel liners and robust structural frames designed specifically for abrasive iron ore and hard rock formations prevalent in North African mining sites.
Standard equipment is manufactured and pre-tested within 30-45 days. We coordinate secure maritime logistics directly to regional ports, ensuring a 100% transport safety tracking mechanism.
Yes. We provide tailored quotation packages including spare parts lists, energy-efficiency ratings, and volumetric throughput analysis based on your project specifications.
Our engineering team is on high alert 24/7. We offer remote digital diagnostics as well as on-site overseas installation and maintenance training by certified mechanical experts.
Contact our engineering consultants today for customized technical drawings, product catalogues, and official pricelists.
Send Inquiry Now